Email
WhatsApp

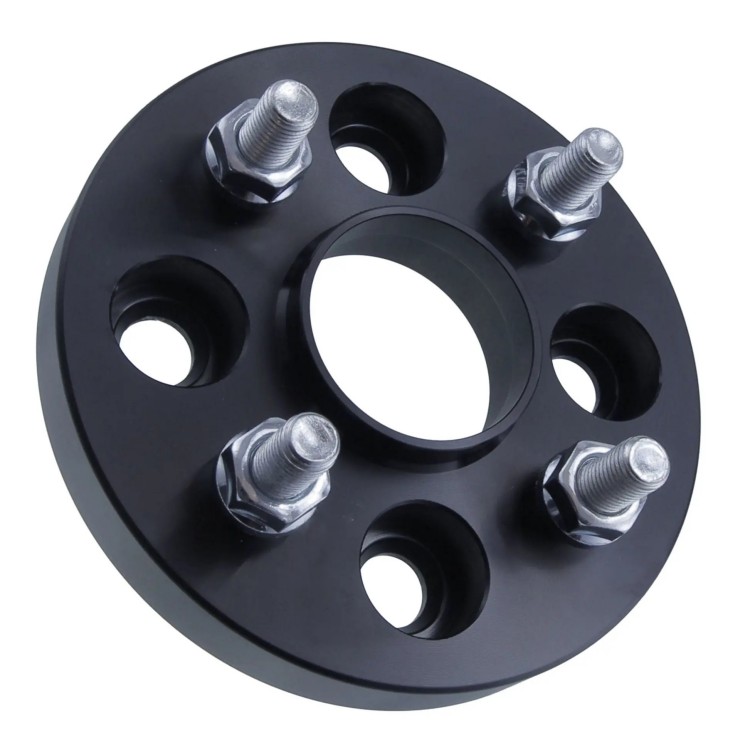
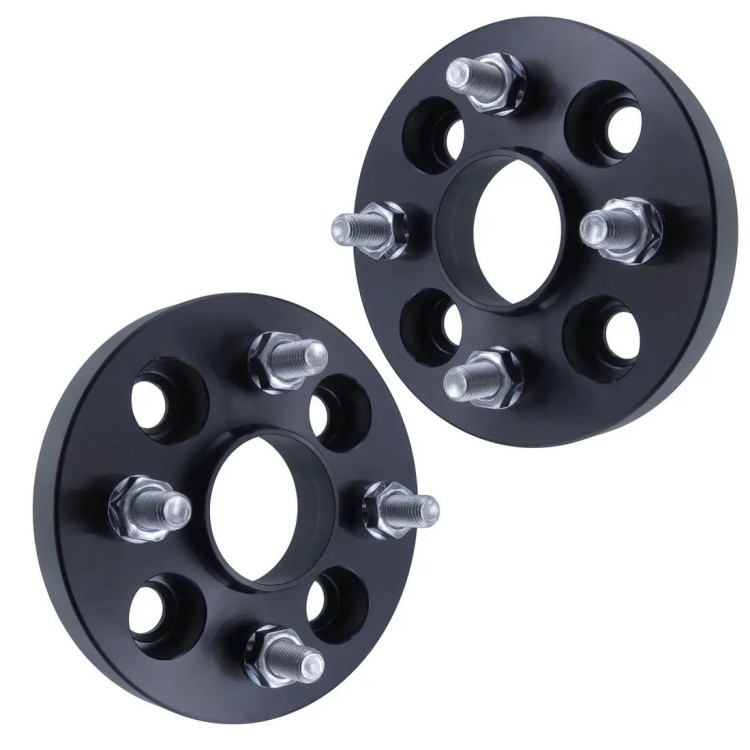
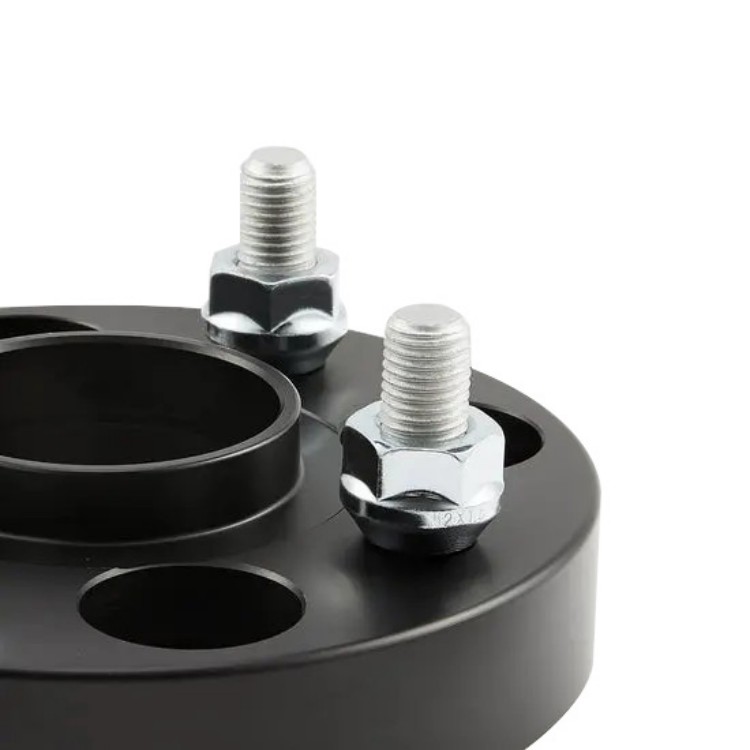
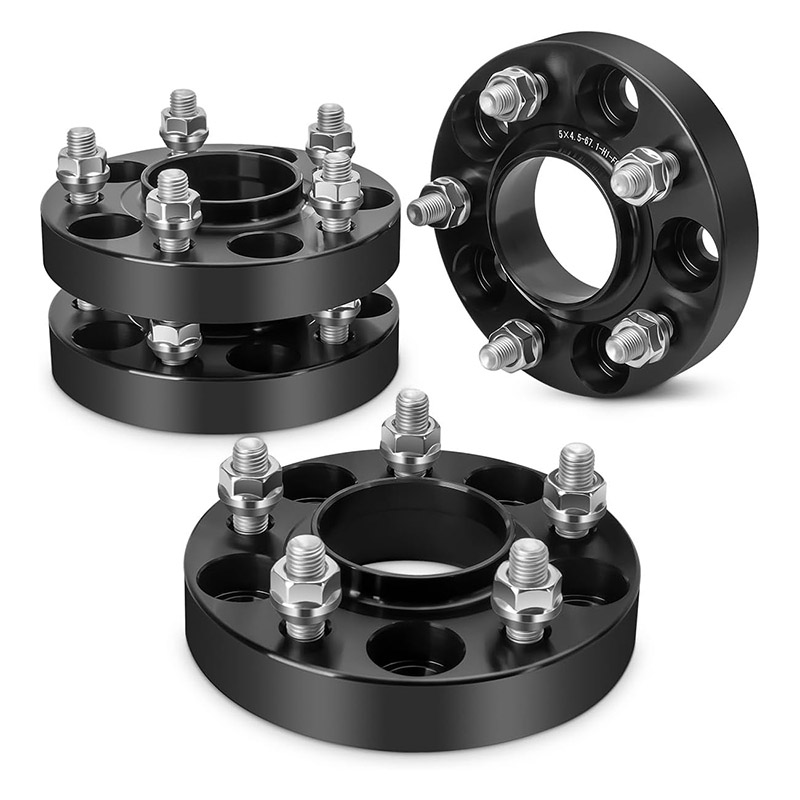
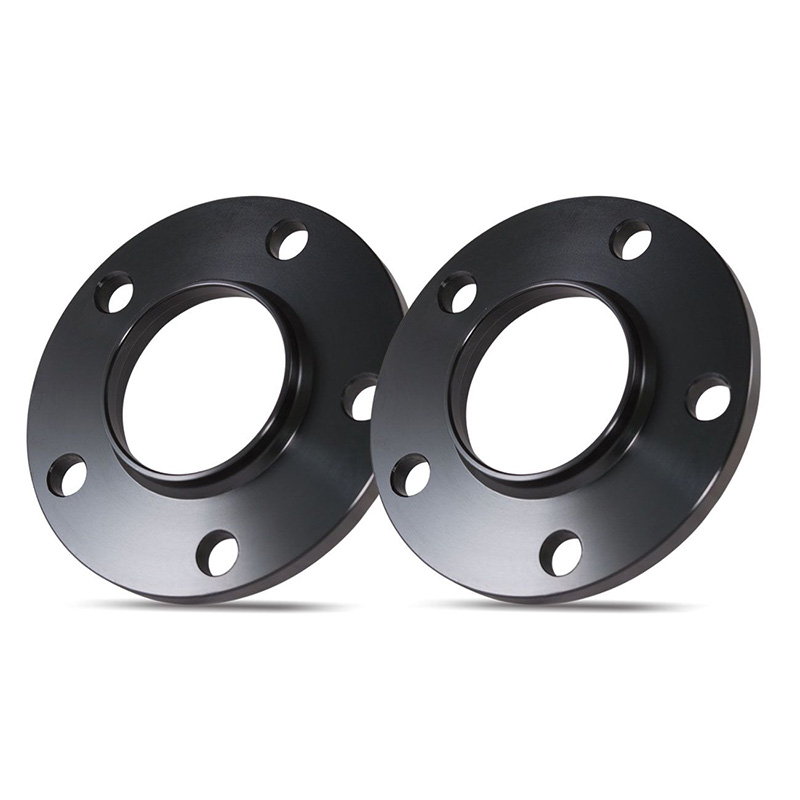
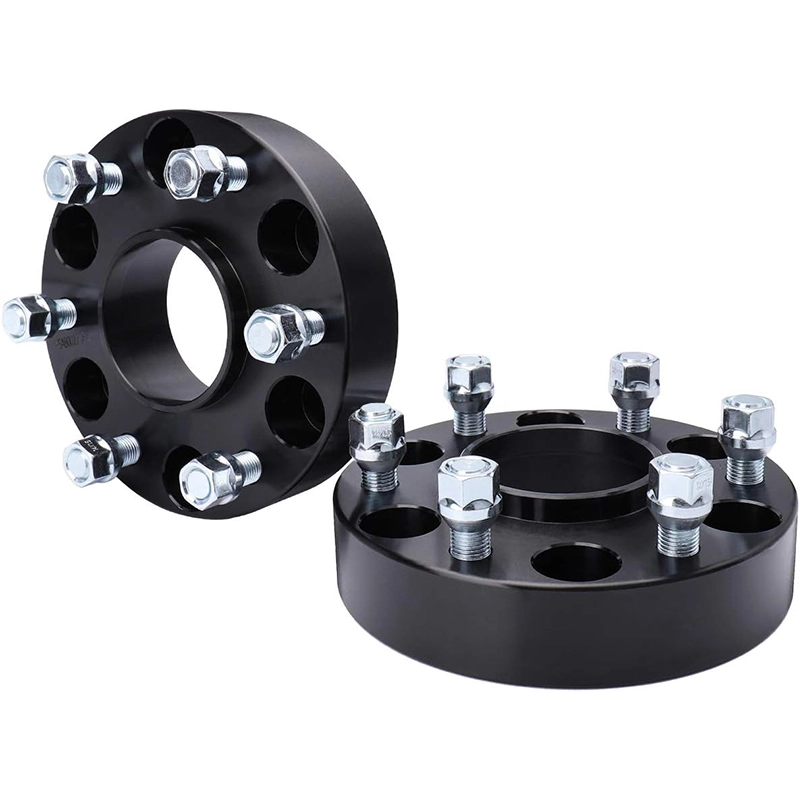
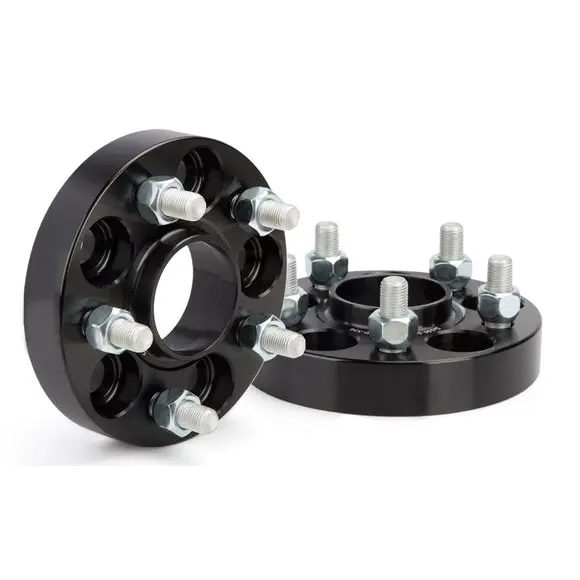
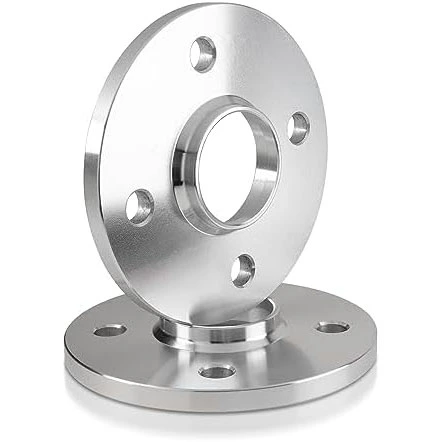
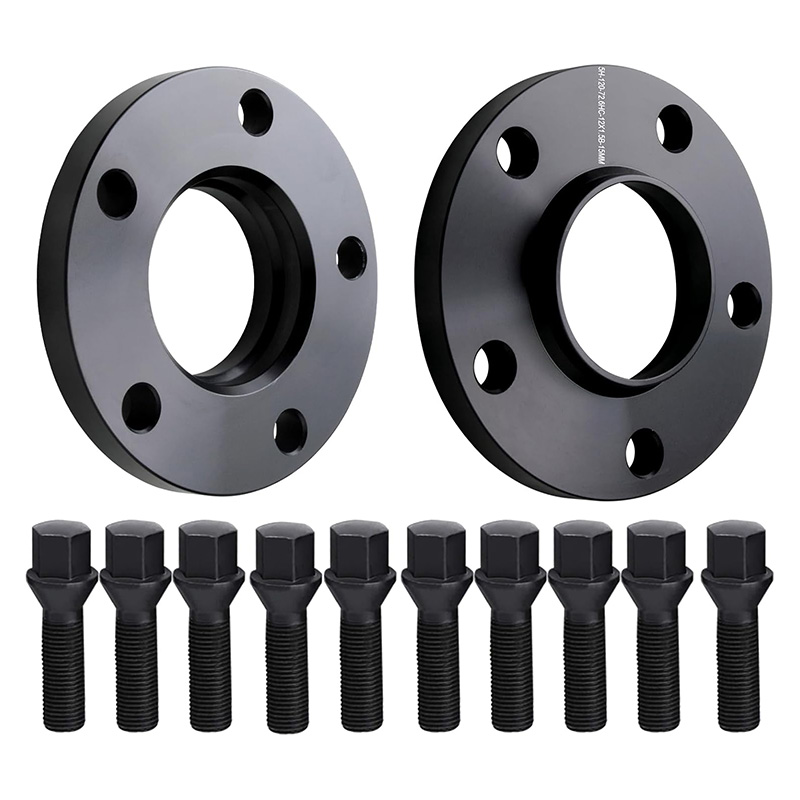
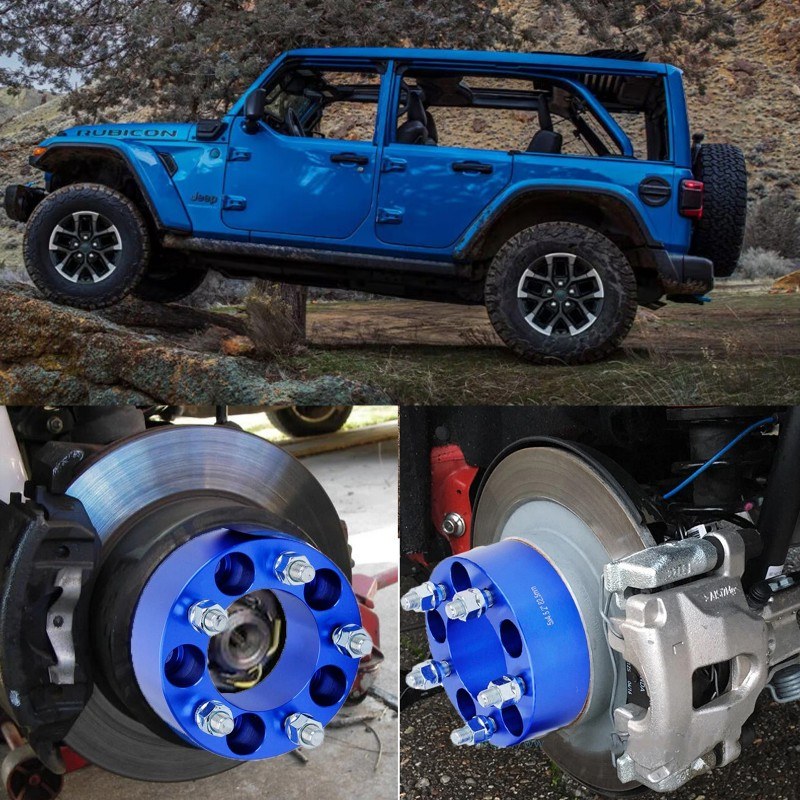
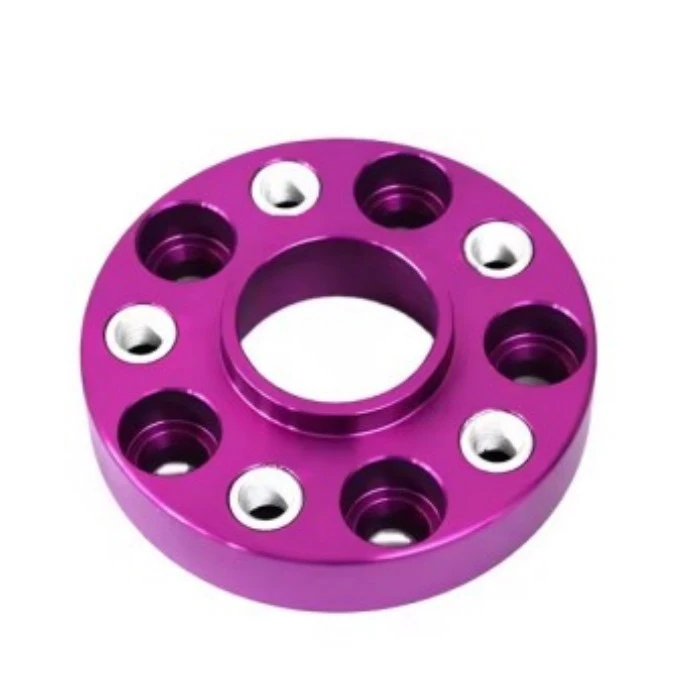
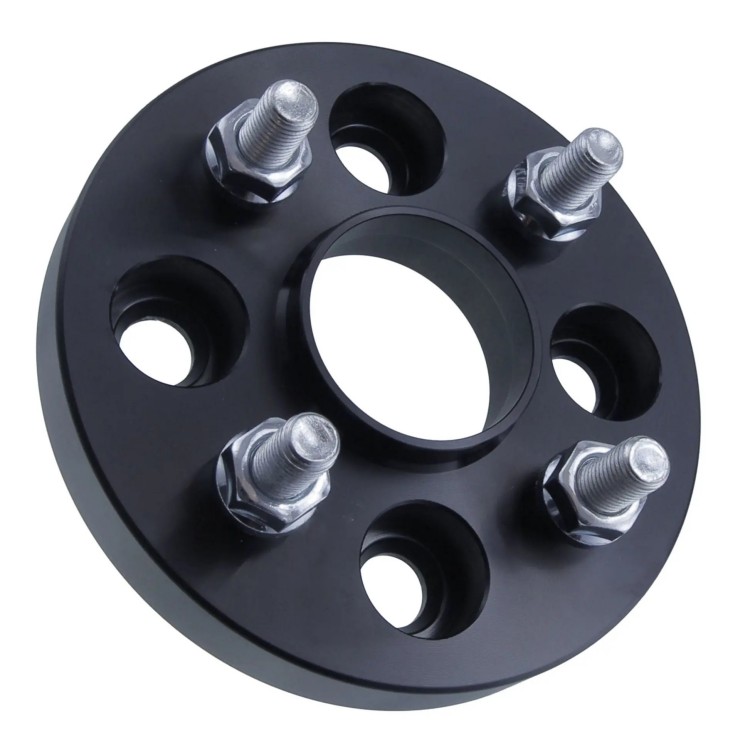
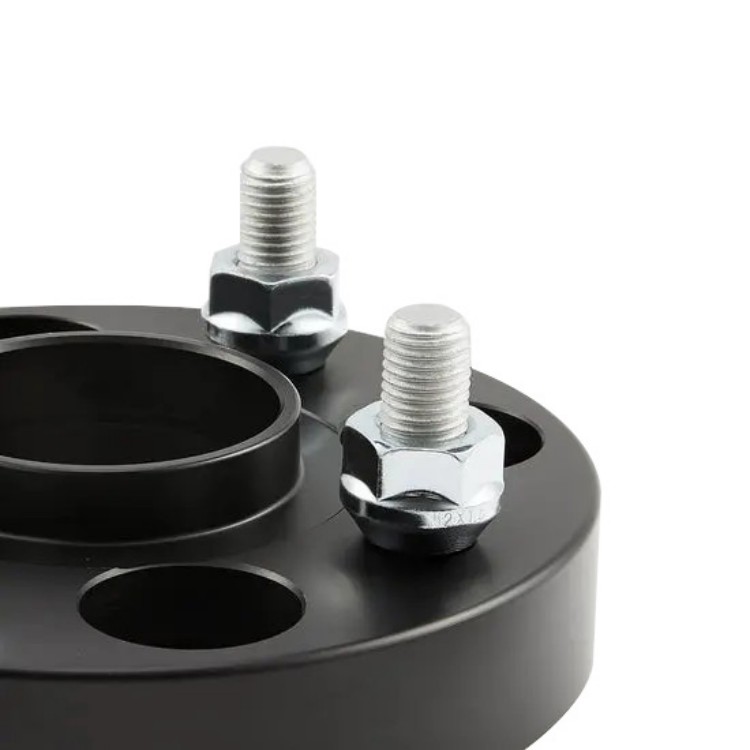
The PCD 4x100 CB60.1 Wheel Spacer Adapter is engineered to improve cornering stability, correct wheel offset, and provide essential clearance for aftermarket big brake kits. Manufactured from forged 6061-T6 or 7075-T6 aluminum alloy, this hubcentric adapter increases track width while maintaining precise center bore alignment to minimize high-speed vibration. As a factory-direct manufacturer in China with in-house CNC machining, we deliver chassis components manufactured to meet SGS and TUV testing standards for automotive styling brands, wholesalers, and tuning distributors.
Unlike cheap cast spacers that suffer from micro-porosity and cracking, our forged adapters feature a true hubcentric lip. This lip transfers vehicle load directly to the hub rather than relying solely on wheel studs, protecting chassis geometry and stabilizing handling under aggressive cornering.
|
Item |
Value |
|
Product Name |
PCD 4x100 CB60.1 Wheel Spacer Adapter |
|
Brand Identity |
J&W Auto Parts |
|
PCD (Bolt Pattern) |
4 x 100 mm |
|
Center Bore (CB) |
60.1 mm (True Hubcentric Design) |
|
Material Matrix |
Forged Aluminum Alloy 6061-T6 / 7075-T6 Options |
|
Manufacturing Tech |
Hot-Forged Blank + Multi-Axis Precision CNC Machining |
|
Machining Tolerance |
Under 0.02 mm (Ensures perfect parallel seating faces) |
|
Thickness Options |
15mm, 20mm, 25mm, 30mm (Customizable up to 50mm — common street use: 15-20mm; track/widebody: 25mm+ ) |
|
Integrated Studs / Class |
Grade 10.9 or 12.9 Carbon Steel Studs (Pre-installed) |
|
Thread Pitch Options |
M12x1.25 / M12x1.5 / Custom Pitch |
|
Surface Treatment |
Deep Anodized Black / Anodized Silver / Custom Corrosion Colors |
|
Certification Metrics |
Manufactured to meet SGS and TUV testing standards (Test reports available upon request) |
|
Warranty |
12 Months (Under normal operating and torque conditions) |
|
HS Code |
8708709000 |
|
Lead Time / Capacity |
45 Days / 50,000 pieces per month |
|
Port & Payment |
Port of Ningbo / T/T (30% deposit, 70% before shipment) |
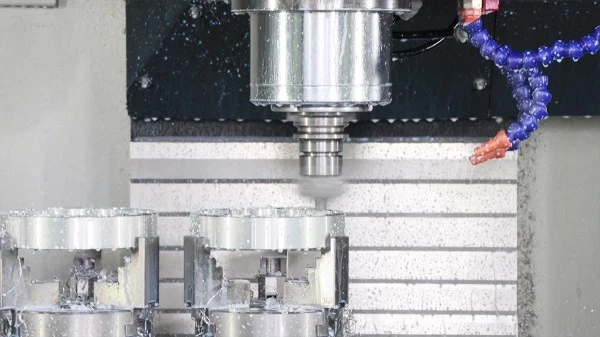
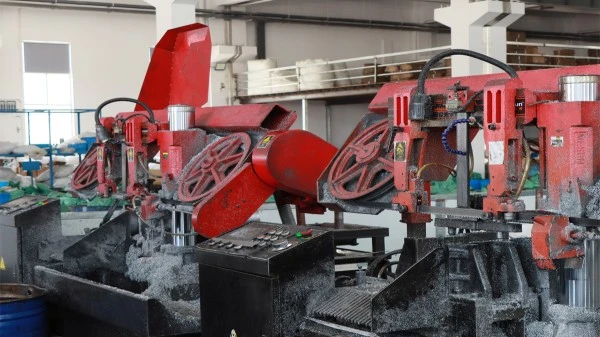
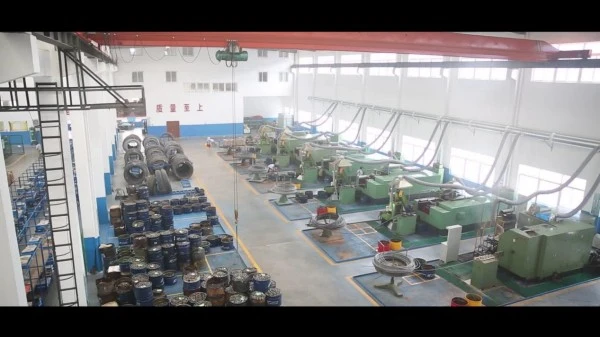
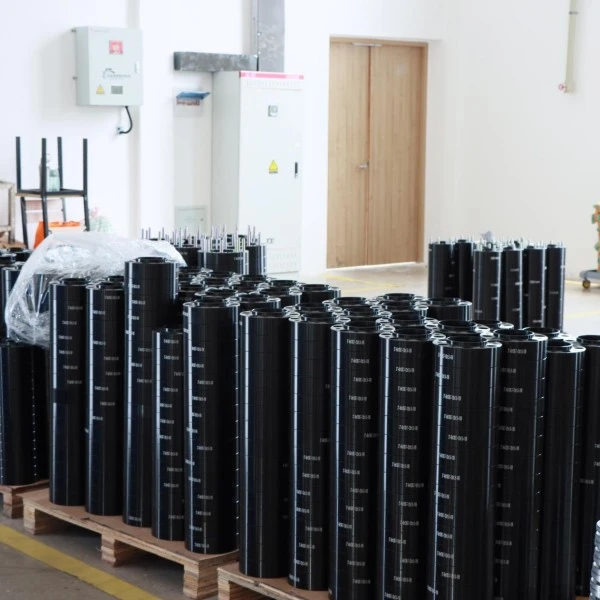
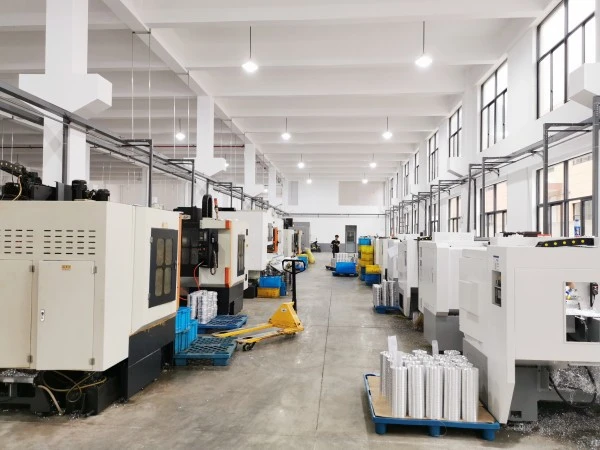
J&W Auto Parts is a professional China manufacturer specializing in forged wheel spacers, wheel adapters, lug nuts, and automotive fastening components. Operating from our own specialized industrial facility in Ningbo, Zhejiang, we combine advanced mechanical forging with multi-axis machining to manage the entire lifecycle from raw metal billet procurement to final surface treatment.
Our 20-Year Manufacturing Journey:
· 2006 – Foundation: Started as a precision tool & die shop in Ningbo, focusing on metal cold heading and heavy machining centers for tier-2 automotive fasteners.
· 2016 – Infrastructure Expansion: Expanded factory footprint to over 10 acres, employing over 100 specialists and integrating 12 large cold heading machines and 20 CNC machining centers.
· 2020 – Advanced Surface Lines: Launched our proprietary fully automated electroplating and anodizing production lines, achieving standard-compliant chemical conversions entirely in-house.
· Present Day: Positioned as a premier manufacturing partner delivering custom wheel spacer engineering and high-durability chassis accessories for international distribution networks.
Our adapter features a precision-machined 60.1mm center bore lip that acts as an exact extension of the stock car hub. By locking the wheel centralized onto the hub center rather than relying on lug nuts for alignment, this configuration distributes vehicle weight evenly and minimizes highway wheel wobble.
We reject standard cast iron or low-grade scrap aluminum recasts. Our factory processes solid blocks of hot-forged automotive-grade aluminum alloy. Forging closes internal air pockets and aligns the metal grain structure, reducing unsprung weight while offering high structural yield limits under extreme track stress.
Every adapter undergoes an electro-chemical anodizing treatment. This chemical surface conversion creates a hard oxide outer layer that blocks air and winter road salt moisture, preventing galvanic corrosion between the aluminum adapter and the steel vehicle hub.
To secure a reliable B2B safety profile, our adapters come pre-assembled with heavy-duty metric wheel studs. These fasteners pass strict dynamic balancing and material fatigue testing, providing consistent thread clamping torque and reducing the risk of stud fatigue failure over long-term use.
Cheap "lug-centric" spacers have no center lip — the wheel is centered only by lug bolt tension. Over time, potholes and braking loads shift the wheel off-center, causing steering vibration and high shear stress on studs.
Our hubcentric design solves this. The 60.1mm bore fits tightly onto the hub axle, and the integrated outer nose fits snugly into the wheel's center pocket. The load rests on the hub infrastructure, not the studs.
With over a decade of deep involvement in international trade corridors, we have developed robust logistical workflows tailored to the compliance standards of major regional markets:
· North America: Supplying major wholesale warehouse grids across the United States and Canada. Our Grade 10.9/12.9 studs are engineered to withstand the aggressive winter liquid de-icers (calcium chloride) common in midwestern and northern regions.
· Western Europe: Providing tight-tolerance parallel seating faces (under 0.02mm) that meet the strict mechanical safety expectations of tuning networks in Germany, the UK, and France.
· Oceania: Delivering deep anodized surface layers tested in coastal salt-heavy distribution networks throughout Australia and New Zealand.
· Emerging Aftermarkets: Catering to growing performance stance demands across South America, Southeast Asia, and the Middle East with highly flexible low-MOQ contract runs.
Case Study 1: Aftermarket Wheel Wholesaler (Toronto, Canada)
· The Challenge: A major Canadian wheel distributor faced high return rates (approx. 4.2%) from customers complaining of highway steering wheel wobble at 75 mph caused by uneven tolerances in universal slotted spacers.
· Our Solution: We supplied our custom-branded, CNC-machined PCD 4x100 CB60.1 hubcentric adapters. We locked the parallelism tolerance under 0.02mm and provided customized bulk corrugated packaging ready for retail shelves.
· The Result: The customer reported a noticeable reduction in vibration-related returns after switching to hub-centric adapters.The wholesaler expanded their yearly contract to include our custom-tinted matte black finish series.
Case Study 2: Performance Tuning & Stance Shop (Stuttgart, Germany)
· The Challenge: A track day customization shop needed to clear Brembo big brake kits on a fleet of modified compact sports hatches using 4x100 configurations. Standard spacers were failing shear stress checks under hard track cornering.
· Our Solution: We engineered a dedicated custom thickness batch (22mm) utilizing hot-forged 7075-T6 alloy with a tensile strength yield of 570 MPa, combined with custom laser engraving of the shop's private label brand name.
· The Result: The shop reported flawless performance over multiple track seasons, utilizing the visual thread verification of our open-end design to guarantee fast, safe wheel assembly checks in the pits.
|
Engineering Factor |
J&W Forged 6061-T6 Adapter |
J&W Forged 7075-T6 Adapter |
Cheap Cast Slotted Spacers |
|
Material Substrate |
Forged 6061-T6 Aircraft Aluminum |
Forged 7075-T6 High-Yield Alloy |
Low-Grade Cast Recycled Scrap |
|
Tensile Strength Yield |
Approx 310 MPa (Standard Street) |
Approx 570 MPa (Heavy Track/Race) |
Low (Highly brittle under torque) |
|
Hub Alignment Mode |
True Hubcentric Lip (60.1mm) |
True Hubcentric Lip (60.1mm) |
Universal Lugcentric Slotted Holes |
|
Thickness Tolerance |
Under 0.02 mm Parallel Bounds |
Under 0.02 mm Parallel Bounds |
Poor (Causes uneven wheel seating) |
|
High-Speed Vibration |
Minimized (Perfect center lock) |
Minimized (Perfect center lock) |
High Risk (Prone to axial wobble) |
|
B2B Sourcing ROI |
High (Cost-effective daily use) |
Exceptional (Premium tuning demands) |
Low (Subject to crack replacements) |
Our workshop operates under strict 5S management. Here is how your order moves through our manufacturing steps:
Forged Aluminum Ingot Inspection ➔ CNC Lathe Turning ➔ Multi-Axis CNC Drilling
↓
Final Pallet Packaging ➔ Thread & Tolerance Verification ➔ Anodizing Line ➔ Dynamic Balance Test
1. Forged Aluminum Ingot Inspection: We verify the alloy composition, internal density, and tempering (T6 grade) of raw 6061/7075 aluminum logs before cutting.
2. CNC Lathe Turning: High-precision CNC lathes shape the outer diameter and turn the exact 60.1mm center bore step, maintaining parallelism tolerances under 0.02mm.
3. Multi-Axis CNC Drilling: Automated machining centers drill the 4x100 pitch circle holes and stud pockets simultaneously to ensure absolute true center positioning.
4. Dynamic Balance Testing: Finished adapter blanks undergo spin testing to eliminate mass deviations, ensuring smooth rotation at high tracking speeds.
5. Anodizing Production Line: Adapters pass through our fully automated tanks to receive a uniform, corrosion-resistant black or silver protective finish layer.
6. Thread & Tolerance Verification: QA technicians use precision micrometer calipers and Go/No-Go thread gauges to inspect the seat taper and stud fitment.
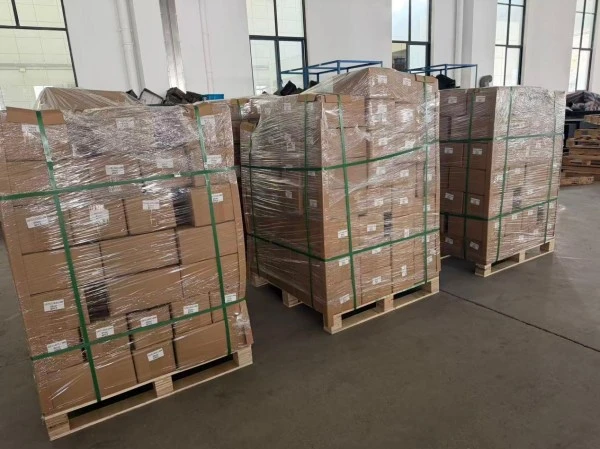
7. Final Packaging: Adapters are clean-sorted, bundled with matching lug nuts if specified, and secured into thick corrugated boxes ready for sea transport from the port.
We help distributors, wholesalers, and private brands create customized retail or commercial product lines:
Production Drawing Confirmation ➔ Sample Approval ➔ Mass Production
· Production Drawing Confirmation: Our engineering team generates detailed 2D/3D blueprints based on your custom thickness requirements, target thread pitches, or private brand logo files before production.
· Sample Approval: We make physical pre-production aluminum samples and mail them to your office. You can test the fitment, anodizing depth, and thread matching yourself before placing the bulk order.
· Mass Production: Once you sign off on the sample, our production facility lines start the forging and CNC tooling cycles to deliver a matching batch.
· Custom Finishes: Available in custom anodized colors and laser engraving of corporate branding.
|
Package Level |
Quantity |
Specification / Details |
|
Inner Box |
2 pcs (1 Pair) per pair |
White or branded interior box. Thickness pairs must match. |
|
Master Carton |
20 pcs (10 Pairs) |
Double-wall corrugated export master box |
|
Carton Size |
42 x 32 x 22 cm |
Standard sizing optimized for container loading grids |
|
Net / Gross Weight |
14.5 kg / 15.5 kg (Varies slightly by thickness options) |
Verified clean weight data for customs clearance |
|
Pallet Logistics |
Available |
Fumigated ISPM-15 standard wooden pallets wrapped with film |
While we focus on internal quality controls over external marketing certifications, our standards are rigorous: 100% raw material inspection, hourly in-process thread checks, and mandatory 72-hour salt spray testing on every batch. We let our product performance speak for itself. Our quality assurance team checks thread tolerances every hour on the floor, and we issue our own internal Material Reports and 72-Hour Salt Spray Testing Logs before any container is sealed for export. If any batch fails our internal inspection standards, it will not be released for shipment. We stand behind our quality.
To avoid purchasing mismatched inventory that could delay your logistics or impact vehicle safety, check these four parameters:
This specific adapter utilizes a 4x100mm setup. It matches 4-lug hubs where the distance across opposing bolt circles measures exactly 100mm. It is a standard application for small platforms like Renault Clio/Megane, Nissan Micra/Note, and select Toyota compacts.
The 60.1mm bore must match the vehicle axle snout exactly. If the car's factory hub snout is larger than 60.1mm, the adapter will not sit flush against the rotor brake face. If the snout is smaller, you will require hubcentric rings to close the tolerance gap safely.
Measure the distance from the outer tire sidewall to the inside edge of the fender lip. Choose a thickness (e.g., 15mm or 20mm) that clears the inner fender without forcing the tire tread to rub against the outer sheet metal during full suspension travel.
Ensure the pre-installed studs on the adapter (such as M12x1.25 or M12x1.5) match the factory lug nut thread pattern of the target vehicle. Mixing thread pitches will strip the internal threads of your mounting hardware during assembly.
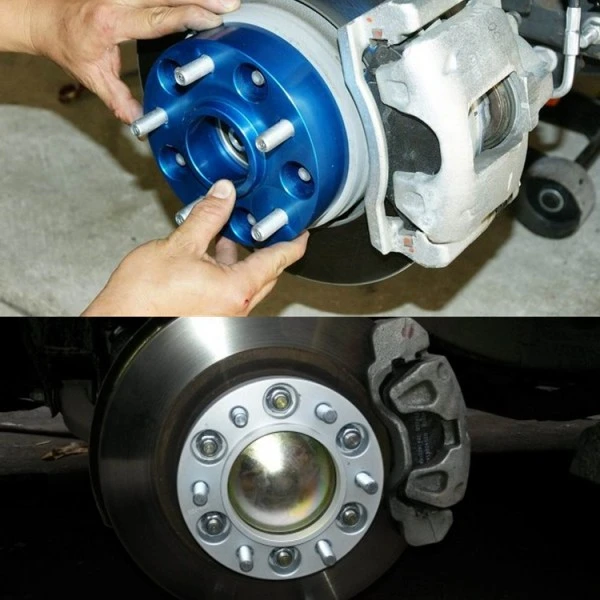
1. Prepare Rotors: Thoroughly clean the vehicle hub face using a wire brush to remove rust scales, old oil, or debris. The adapter face must sit completely flat against the brake rotor face.
2. Mount the Adapter: Slide the 4x100 spacer adapter onto the factory wheel studs. The adapter should sit flush against the hub face.
3. Secure the Adapter: Thread the provided short open-end lug nuts onto the factory studs. Tighten them in a star pattern to the vehicle manufacturer's recommended torque specifications. This locks the adapter firmly to the hub.
4. Mount the Wheel: Place the wheel over the adapter's pre-installed studs. Secure the wheel using your aftermarket lug nuts, tightening in a star pattern to the correct torque.
5. No Impact Wrenches: Never use pneumatic impact wrenches at any stage. Excessive impact can over-stretch studs, crack the alloy seat, and damage the anodized finish.
A: A 4x100 wheel spacer adapter physically extends the wheel mounting surface outward by a specific millimeter thickness on a 4-lug vehicle hub with a 100mm pitch circle diameter. Its primary functions are widening the vehicle track width to optimize cornering stability, correcting incorrect wheel offset (ET) when changing to aftermarket rims, and pushing the wheel spokes outward to create clearance for oversized brake calipers.
A: Yes, hubcentric design is standard for heavy commercial and high-speed passenger safety. A hubcentric spacer features a precision center ring (like our 60.1mm lip) that fits tightly onto the car axle snout and into the wheel bore, centering the entire assembly perfectly. Lug-centric spacers lack this ring, relying entirely on bolt tension for alignment, which frequently allows the wheel to shift off-center under load, leading to severe steering wheel vibration and accelerated stud fatigue.
A: The proper thickness depends on your specific tire-to-fender clearance. To measure, place a straightedge flat against the outer tire sidewall and use a caliper to measure the distance to the inside edge of your fender lip. Choose a thickness option (e.g., 15mm or 20mm) that is slightly less than that gap, ensuring your tires do not scrape the sheet metal under full suspension compression or hard cornering.
A: Yes. B2B wholesale container buyers can easily mix this standard 4x100 specification with other high-demand sizes (such as 5x114.3 or 5x120), as well as our factory-direct cold-headed wheel lug nuts and wheel bolts in a single consolidated container shipped directly from the Port of Ningbo.
A: Absolutely. For any specialized contract manufacturing, custom offset modifications, or private label branding orders, our in-house engineering department generates and confirms detailed 2D/3D technical drawings with the client before tooling any manufacturing lines.
Get your factory-direct quote within 12 business hours — free samples available upon request.
admin@jwautopart.com
Address
No.539 Guangyi Road, Guanhaiwei Town, Cixi, Ningbo, Zhejiang, China
Tel